Cases and experience
Experience from practice. Insight for your organisation.
Strategic choices, organisational development and operational improvement: discover Ronald’s background and the experience that shapes his approach.
Operational experience, from strategy to shop floor.
Ronald is an operations executive with more than 35 years of international experience leading multiple sites in automotive, manufacturing, logistics and FMCG.
He has delivered organisational and operational transformations, M&A programmes, operational footprint optimisation and operational-excellence programmes. Building high-performance cultures, demonstrable business results, international change programmes and sustainable value creation are the common threads throughout his career.
Career highlights
Leadership responsibility
As an executive and board member, COO and shareholder, Ronald took responsibility for strategy implementation, operational governance and sustainability. His practical experience in operational excellence and change management is complemented by speaking engagements and executive coaching.
Strategic initiatives
Ronald delivered operational transformations, footprint optimisation, M&A programmes and post-merger integrations in Europe. He led international teams through growth, restructuring and cultural transformation, both in Europe and across global production networks.
Transformation impact
He delivered cost-reduction and operational-efficiency programmes ranging from several hundred thousand to several million euros. Productivity, safety, quality, customer satisfaction and profitability improved across different industrial sectors.
An improvement culture across a global production network.
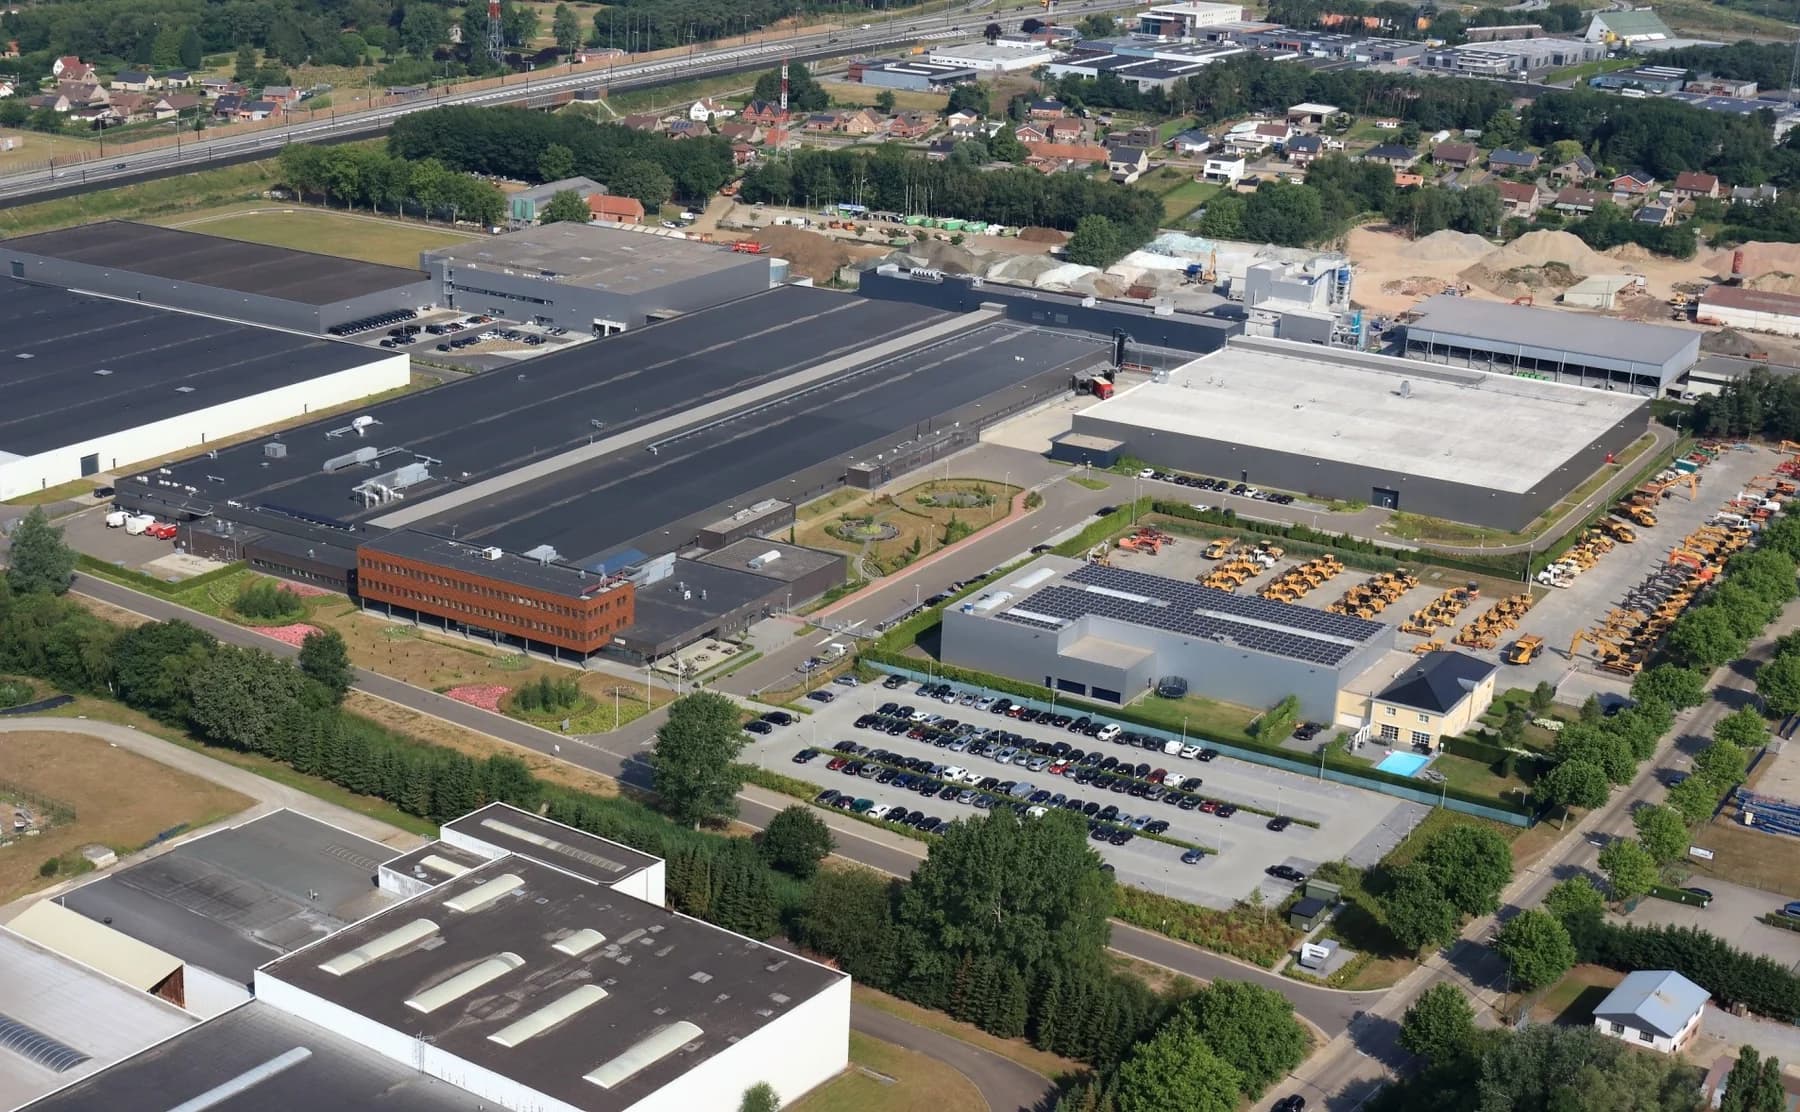
At an international manufacturer in the tobacco industry, Ronald had the opportunity to roll out operational excellence globally. The programme began with a pilot project in a Belgian factory. The initial results demonstrated what a shared approach could mean for other sites.
Board support was an important starting point. The programme focused primarily on the right culture: involving and coaching the right people so they could inspire and guide their local teams. Operational excellence became part of daily decisions and collaboration.
Experience from the pilot project was used to develop the approach further and spread it across the production network. Over four years, this international programme achieved very significant savings through efficiency improvements.
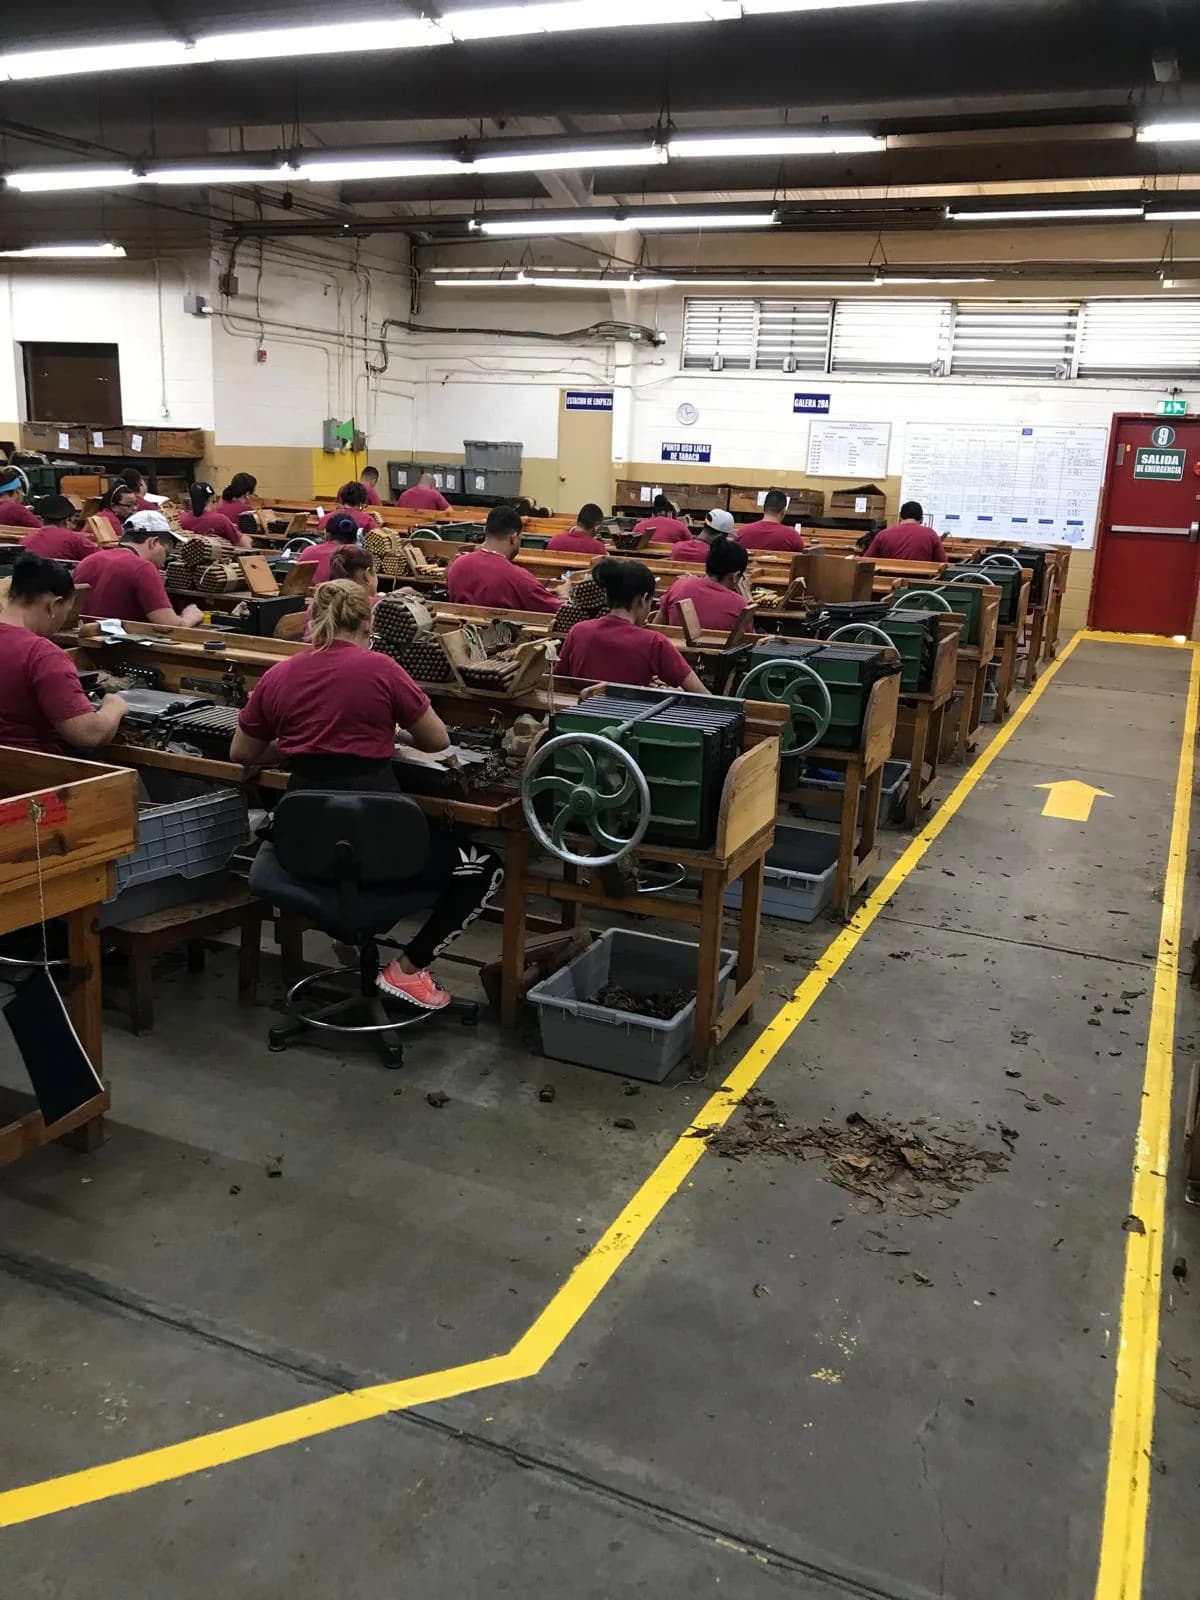
Savings through efficiency improvements within this programme.
Results of the international improvement programme over four years.
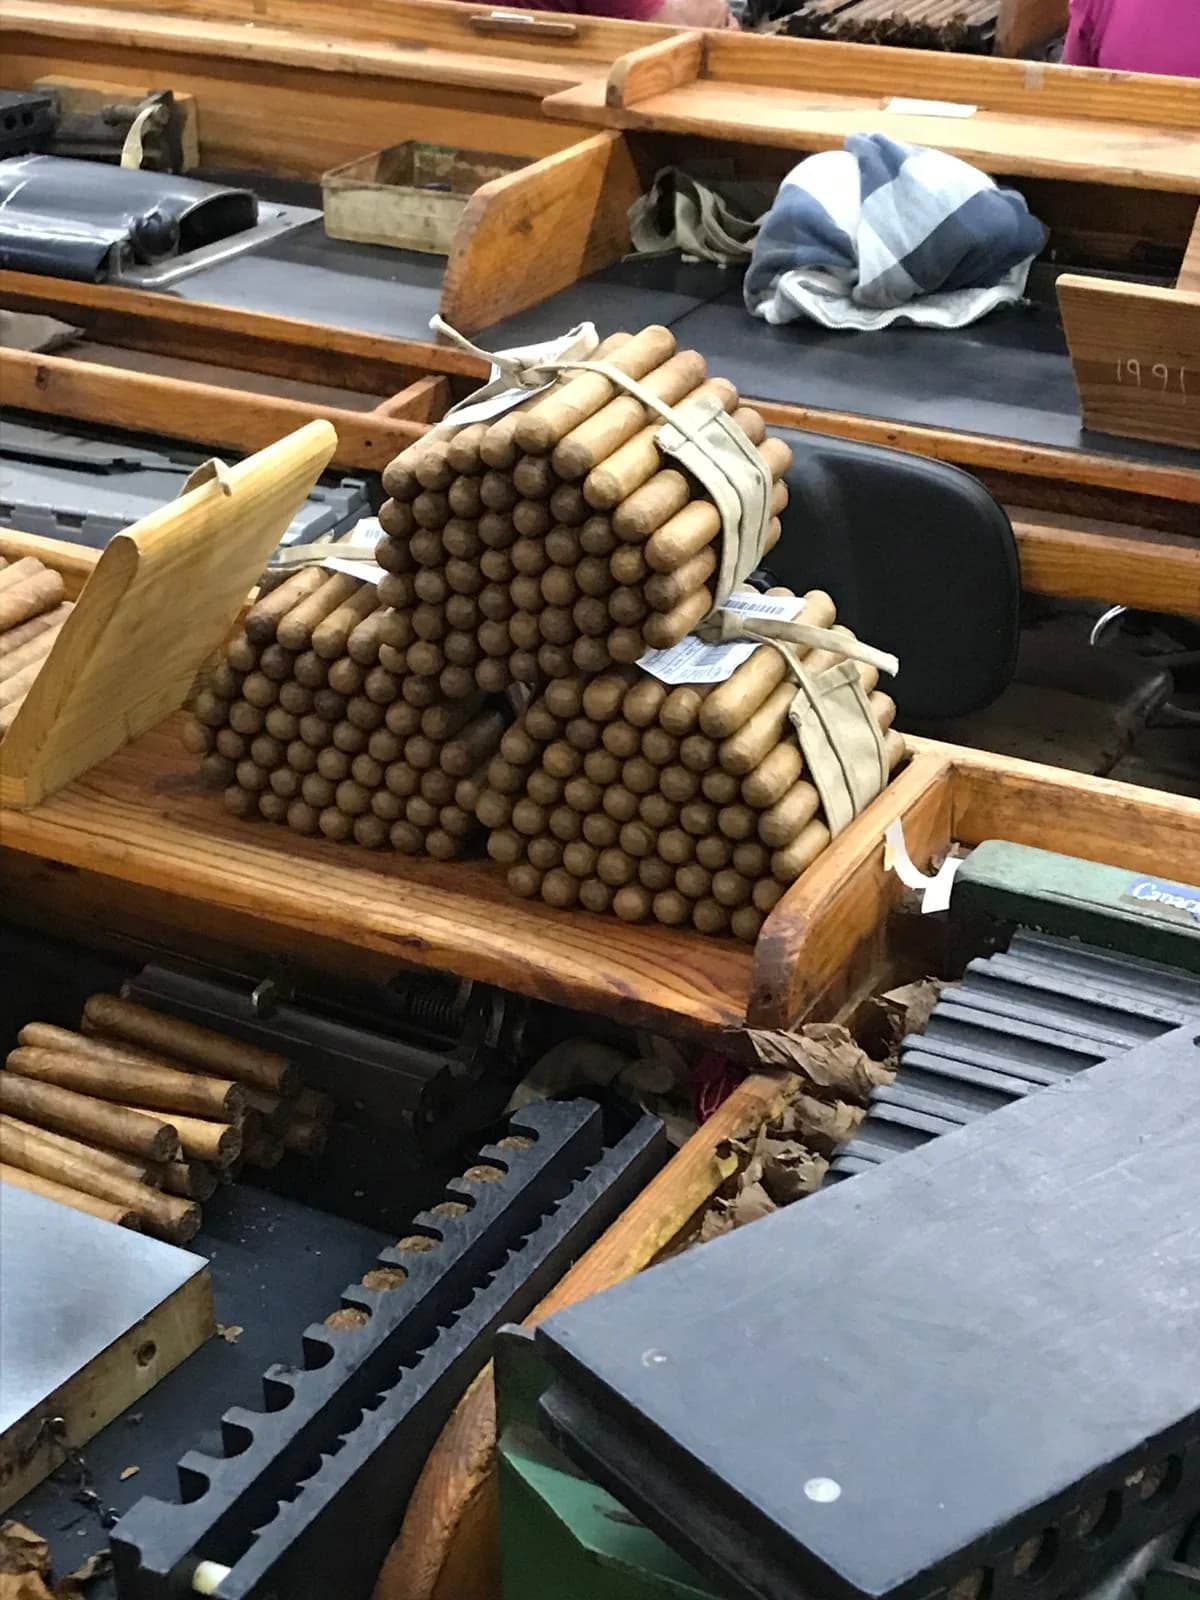
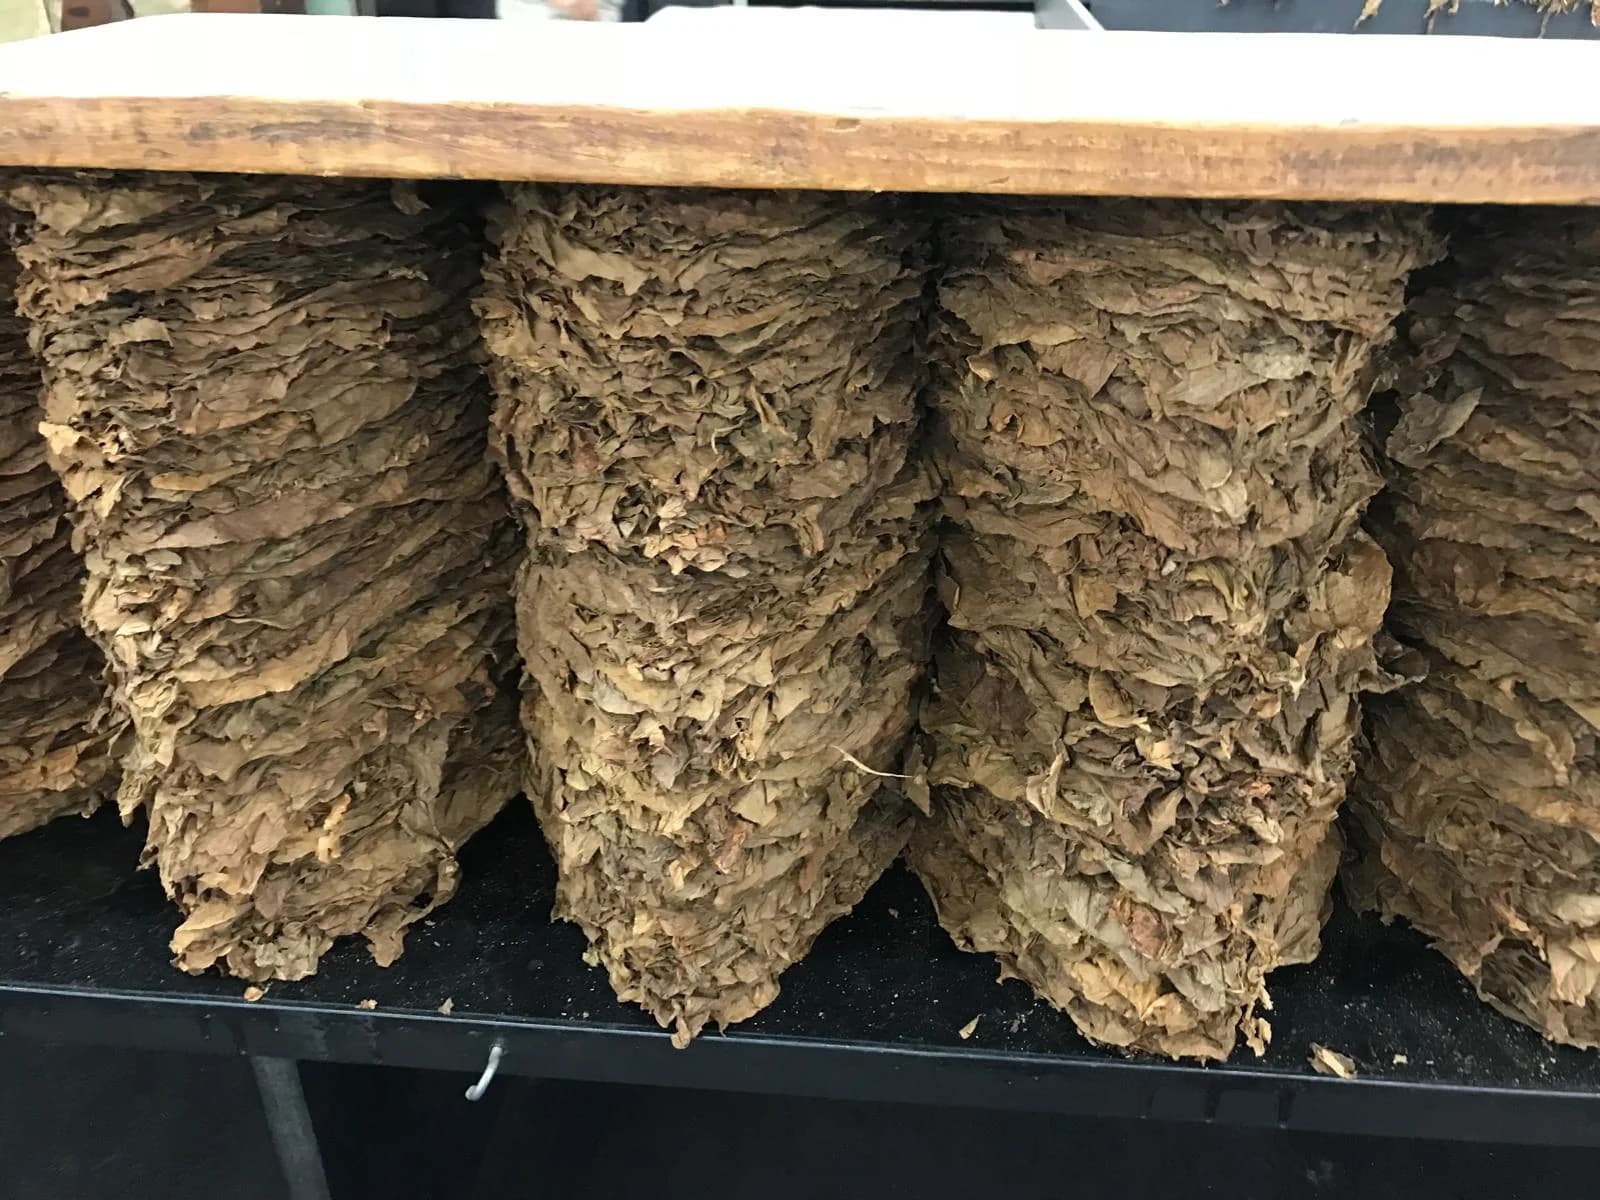
Operational excellence as a common thread across Europe.
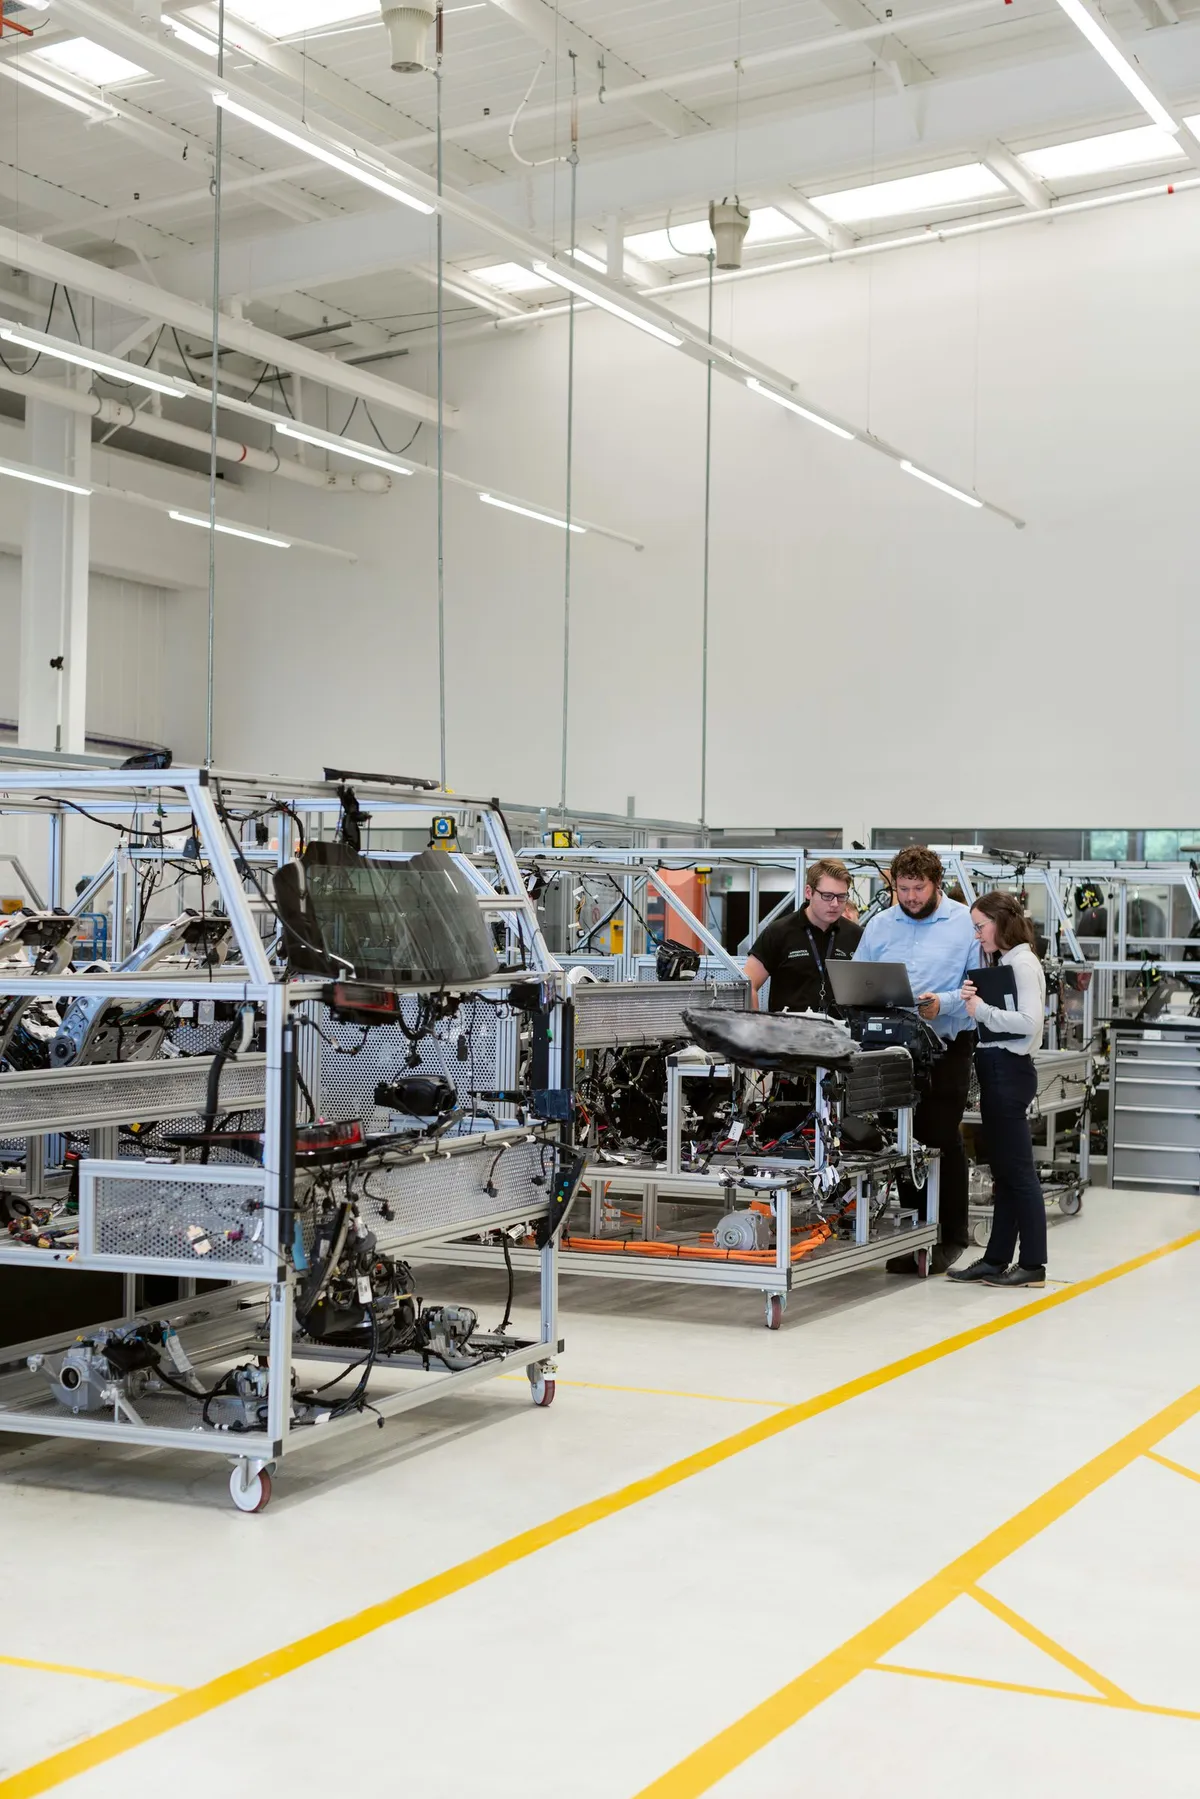
An operational-excellence programme was implemented at all European sites of a Tier 1 automotive supplier. The programme connected a shared direction with the daily practice of individual factories.
Over several years, the organisation developed a culture of visual management, problem solving and Lean Leadership. Managers and employees learned to make deviations visible, investigate causes and take responsibility for improvement. Developing people supported the application of these practices on the shop floor.
- >50%
Fewer lost-time accidents over four years.
- Up to +25%
Productivity improvement across different production lines.
Separate indicators within the automotive programme.
Footprint and operational excellence in logistics.
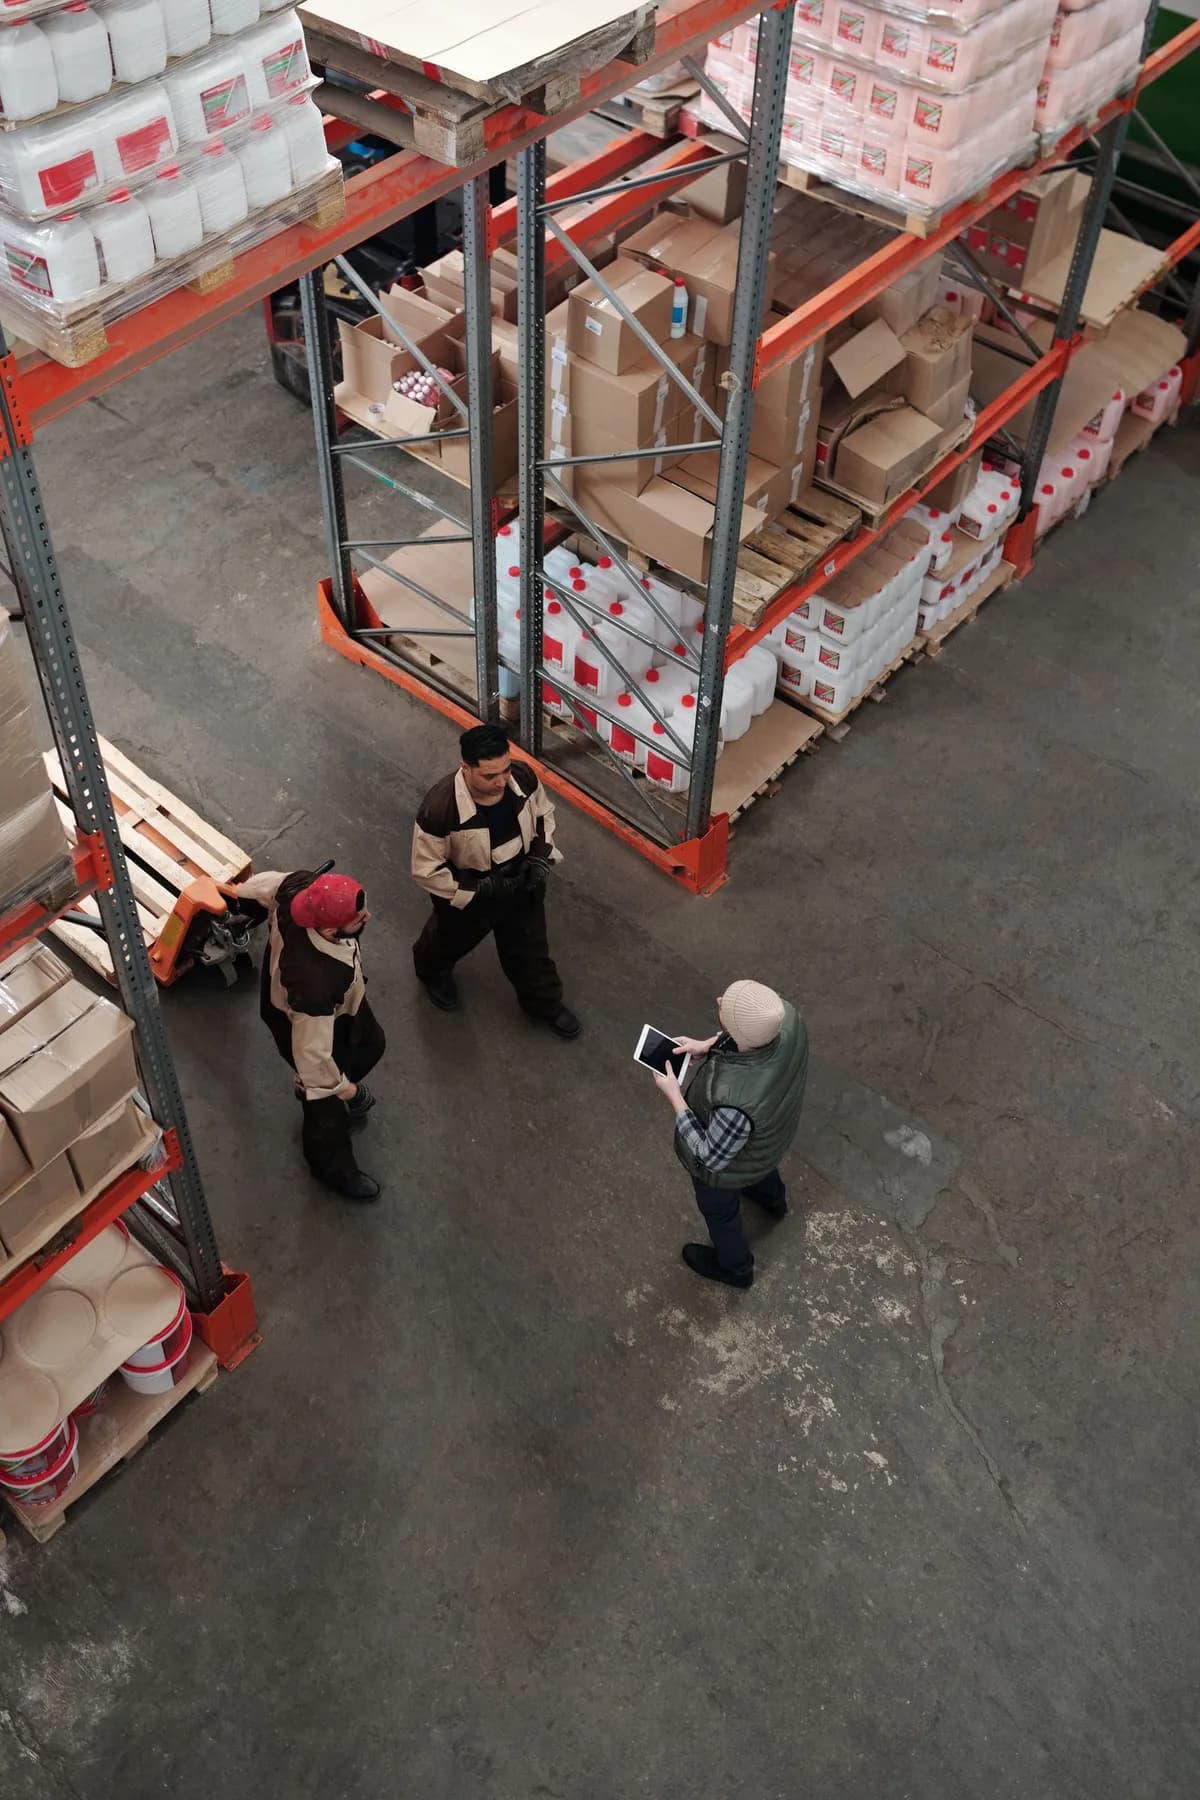
At an international logistics organisation, operating profit and efficiency improved by around 30% over two years. Lost-time accidents fell to zero within that period.
The approach combined operational footprint optimisation with the fundamentals of operational excellence. Decisions about the organisation of activities were connected with daily operations, bringing strategic direction, performance and safety into focus together.
- Around +30%
Improvement in operating profit and efficiency.
- 0
Lost-time accidents at the end of the period.
Results within the logistics programme over two years.
More achievements from practice
New production and warehousing
Launching a new warehouse and production site for a Tier 1 automotive supplier.
International footprint
Developing and implementing international footprint changes at several Tier 1 automotive suppliers.
Efficiency improvements in electronics
More than €1 million in cost reductions through insourcing and efficiency improvements at an electronic components manufacturer.
M&A and integration
Operational support for M&A projects and integrations at several international companies.
Targeted improvement programmes
Separate projects include improving OTIF from 90% to more than 99%, reducing LTIR by more than 50%, increasing output by 10% to 25% and improving Total Cost of Quality by more than 50%. These indicators relate to different programmes and are not added together.
What do you recognise in your organisation?
Tell us what you are facing today and which change you have in mind. This may be a specific operational question or a situation that is not yet entirely clear. In an initial conversation, we explore what needs further attention and which support might fit.
Calling is the most direct way to get acquainted. If you prefer to send a short explanation by email first, that is equally welcome.